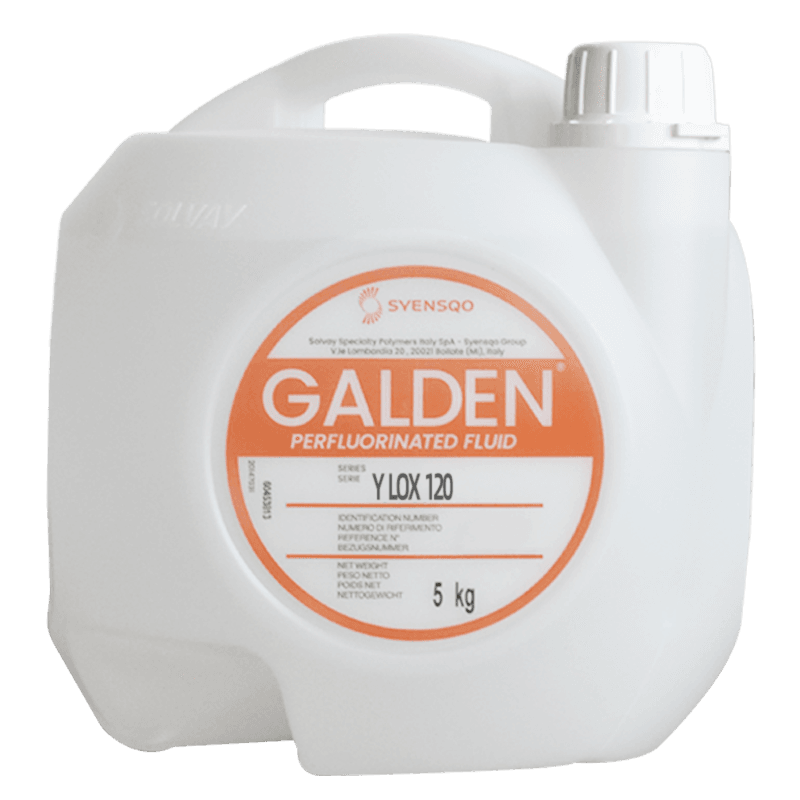
Key Features & Benefits
- Excellent Oxygen Compatibility: It is completely inert in oxygen-enriched or liquid oxygen environments, offering no flash point or auto-ignition point to eliminate fire and explosion risks.
- Outstanding Chemical Inertness: Highly resistant to aggressive chemicals, including strong acids, alkalis, chlorine, fluorine, organic solvents, and petroleum-based fuels.
- Low Vapor Pressure: Minimizes fluid evaporation and backstreaming in high-vacuum or high-temperature environments, preventing system contamination.
- Thermal Stability: Operates reliably across a broad temperature range from -46°C to over 100°C without thermal decomposition.
- Safety & Durability: Non-toxic, hydrolytically stable, radiation-resistant (Gamma rays), and offers a service life multiple times longer than standard mineral oils.
Typical Applications
- Oxygen Generation & Transport: Lubrication for industrial oxygen compressors, valves, regulators, and piping components.
- Vacuum Pumps & Hydraulics: Base fluid for high-vacuum pumps operating in harsh chemical or semiconductor processing environments.
- Corrosive Chemical Handling: Mechanical components exposed to highly reactive gases and corrosive media.
Typical Technical Specifications
- Kinematic Viscosity at 20°C: 120 cSt
- Kinematic Viscosity at 40°C: 42 cSt
- Kinematic Viscosity at 100°C: 6.8 cSt
- Viscosity Index (VI): 120
- Pour Point: -46°C
- Vapor Pressure at 20°C: 2 × 10⁻⁴ torr
- Density at 25°C: 1.890 g/cm³