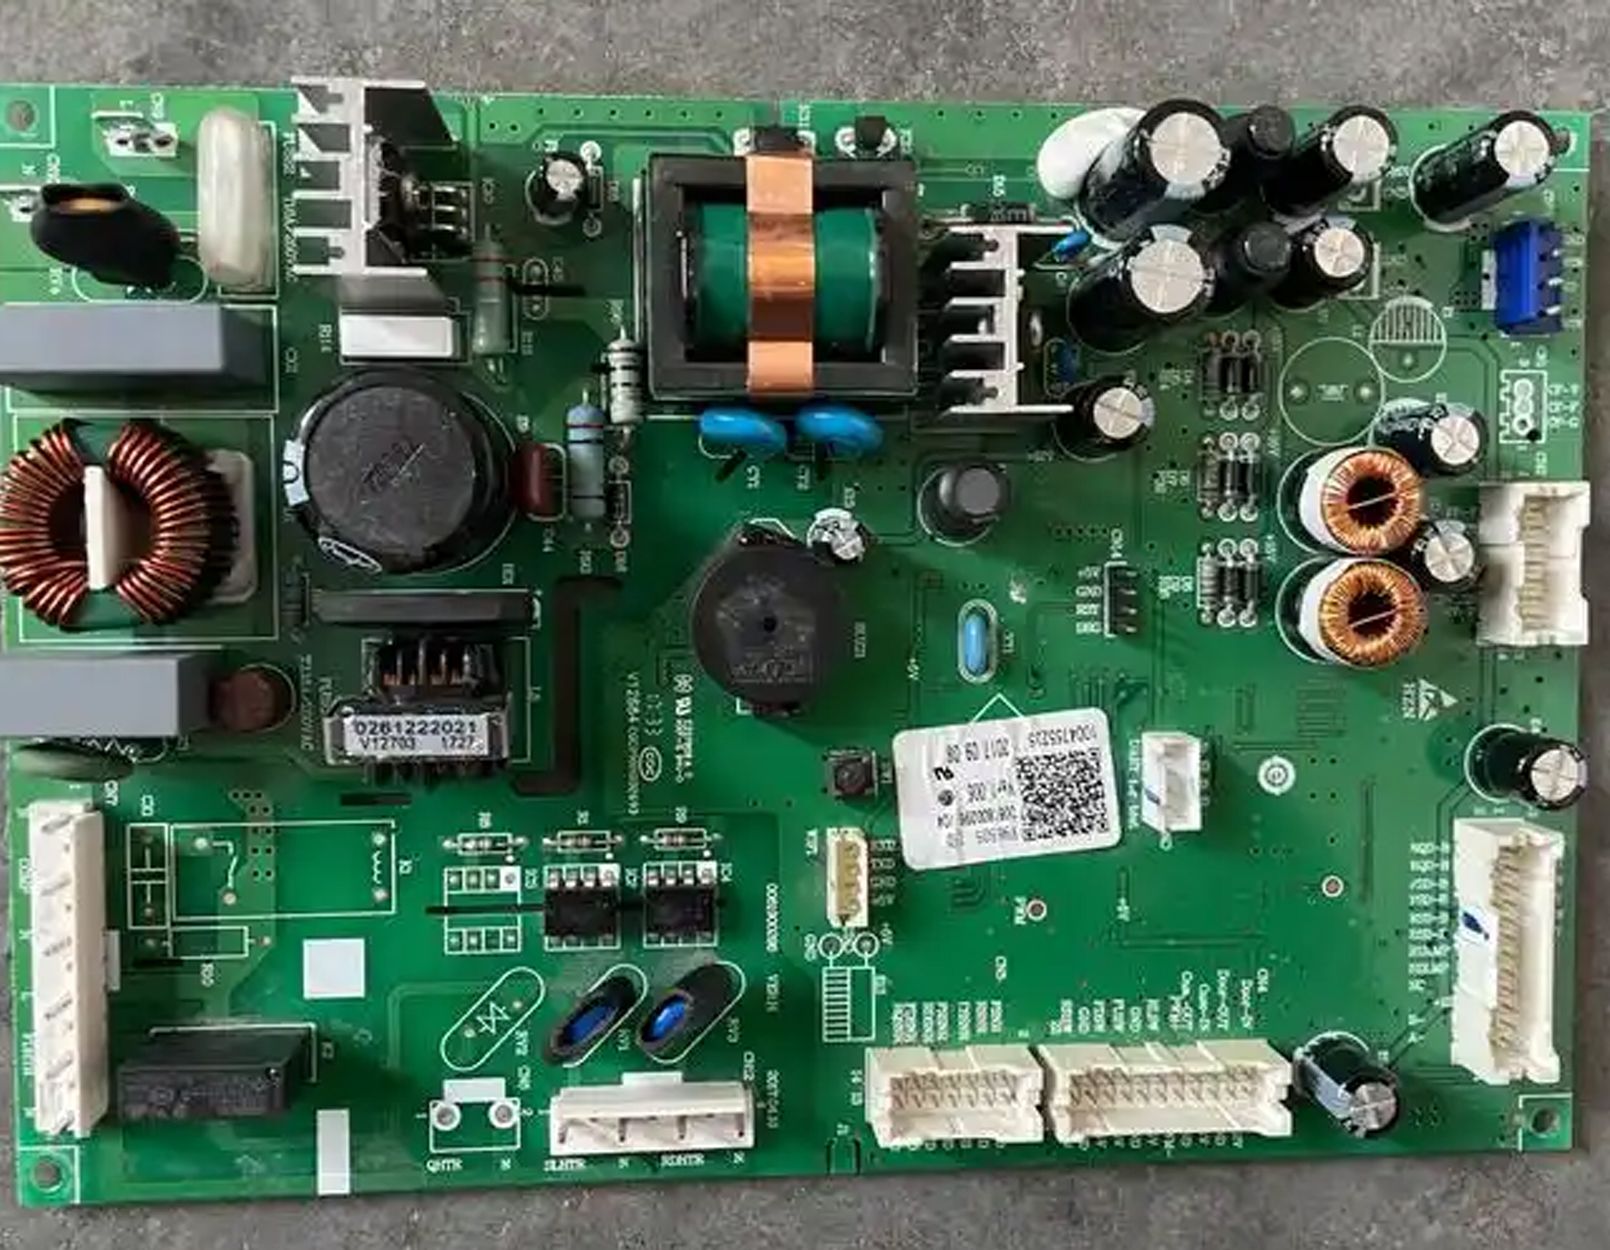
A refrigerator is a complex system in which the circuit board handles various control tasks, such as temperature regulation, defrosting, and automatic diagnostics. Because refrigerators operate continuously, they are susceptible to adverse conditions like moisture and water vapor. Once the circuit board is compromised by moisture, it can lead to issues such as component damage, short circuits, and signal transmission failures, severely affecting the refrigerator's normal operation.
A refrigerator is a complex system in which circuit boards handle various control tasks, such as temperature regulation, defrosting, and automatic diagnostics. Because refrigerators operate continuously, they are frequently exposed to adverse conditions like moisture and water vapor. If circuit boards are compromised by moisture, issues such as component damage, short circuits, and signal transmission failures can occur, severely affecting the appliance's normal operation. To address this challenge, the expert team at Shenzhen Zhongfu has dedicated itself to developing high-performance nano-protective coatings—featuring waterproof, moisture-proof, anti-oxidation, and corrosion-resistant properties—to safeguard refrigerator circuit boards against moisture-related damage.
Principles and Characteristics of Nano-Protective Coatings
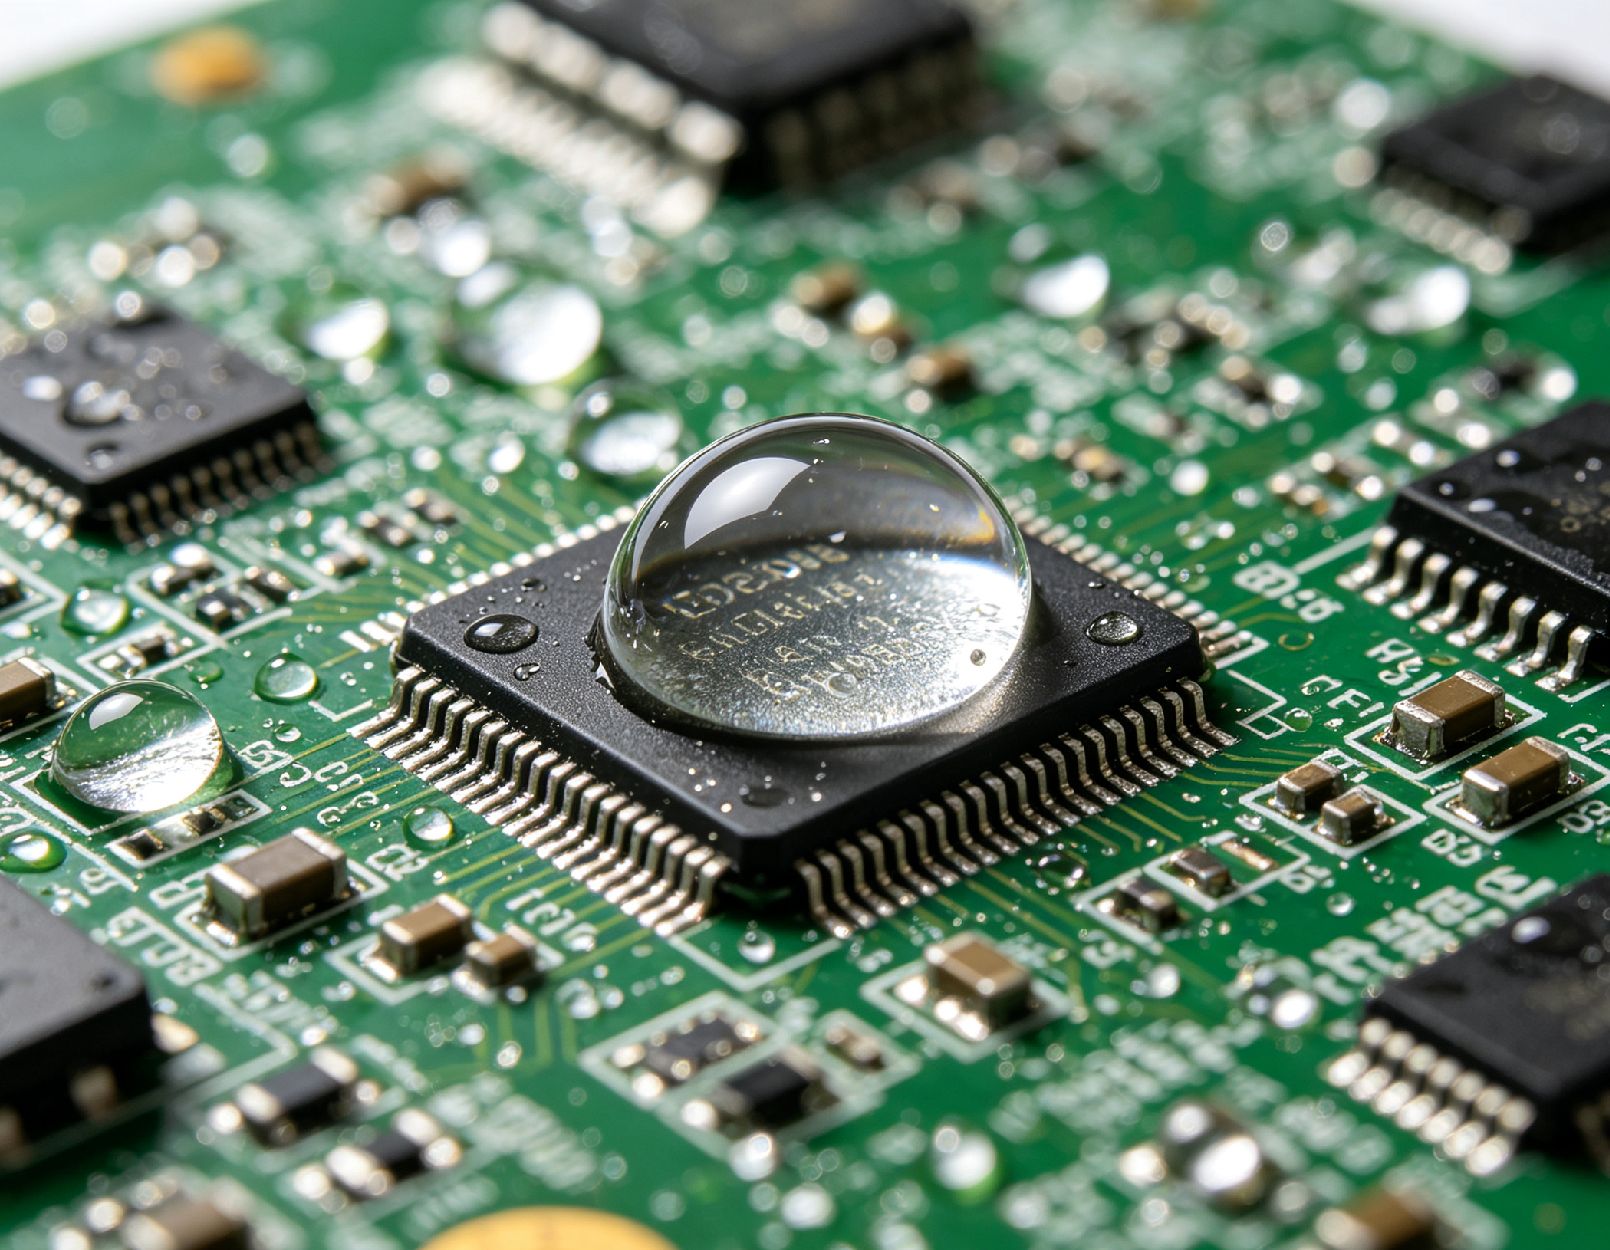
Nano-protective coatings are polymer materials characterized by their ultra-thin, transparent, and eco-friendly nature, making them suitable for a wide range of applications in sectors such as home appliances, telecommunications, and automotive manufacturing. They function by leveraging the unique properties of fluorine—specifically its high surface tension and oxidation resistance. Fluorine particles undergo a series of polymerization reactions and deposit onto the substrate surface, forming a polymer film with a biomimetic structure. The micro- and nano-scale structures on the coating's surface support liquid molecules, preventing direct contact between the liquid and the substrate, thereby providing effective protection.
(1) Ultra-thin: The coating is nanometer-scale in thickness, ensuring no impact on the dimensions or performance of the circuit board;
(2) Transparent: The coating is colorless and transparent, preserving the circuit board's original appearance;
(3) Eco-friendly: The coating material is non-toxic and pollution-free, complying with international environmental standards;
(4) High-performance protection: Offers excellent water resistance, moisture resistance, oxidation resistance, and corrosion resistance;
(5) Durable and stable: Long-term testing has demonstrated the coating's high durability and stability.
Application of Nano-Protective Coatings on Refrigerator Circuit Boards
A professional team has developed a comprehensive application solution for nano-protective coatings tailored to the specific characteristics of refrigerator circuit boards. During production, the circuit board surface is cleaned, and the nano-protective coating is applied evenly using methods such as spraying, dip coating, or vacuum coating. The coating forms an ultra-thin, transparent protective film that blocks moisture ingress and provides oxidation and corrosion resistance, effectively extending the service life of the refrigerator circuit board.
Refrigerator circuit boards utilizing nano-protective coating technology offer the following advantages:
(1) Enhanced product reliability: Water and moisture resistance reduce the risk of circuit board damage, ensuring the refrigerator operates normally;
(2) Extended service life: Oxidation and corrosion resistance mitigate component aging;
(3) Reduced maintenance burden: Effectively lowers after-sales maintenance costs associated with moisture-related issues;
(4) Enhanced brand image: Delivers a superior product experience for consumers and boosts the competitiveness of the company's core products.
Conclusion
Nanoscale protective coating technology offers a durable and highly effective solution for waterproofing and moisture-proofing refrigerator circuit boards. Adopting this advanced technology not only reduces failure rates during operation and extends product lifespan but also boosts user satisfaction, helping home appliance manufacturers gain market share. As a key trend in the future of the home appliance industry, nanoscale protective coating technology is set to play an increasingly important role in this sector.
A refrigerator is a complex system in which the circuit board handles various control tasks, such as temperature regulation, defrosting, and automatic diagnostics. Because refrigerators operate continuously, they are susceptible to adverse conditions like moisture and water vapor. Once the circuit board is compromised by moisture, it can lead to issues such as component damage, short circuits, and signal transmission failures, severely affecting the refrigerator's normal operation.
A refrigerator is a complex system in which circuit boards handle various control tasks, such as temperature regulation, defrosting, and automatic diagnostics. Because refrigerators operate continuously, they are frequently exposed to adverse conditions like moisture and water vapor. If circuit boards are compromised by moisture, issues such as component damage, short circuits, and signal transmission failures can occur, severely affecting the appliance's normal operation. To address this challenge, the expert team at Shenzhen Zhongfu has dedicated itself to developing high-performance nano-protective coatings—featuring waterproof, moisture-proof, anti-oxidation, and corrosion-resistant properties—to safeguard refrigerator circuit boards against moisture-related damage.
Principles and Characteristics of Nano-Protective Coatings
Nano-protective coatings are polymer materials characterized by their ultra-thin, transparent, and eco-friendly nature, making them suitable for a wide range of applications in sectors such as home appliances, telecommunications, and automotive manufacturing. They function by leveraging the unique properties of fluorine—specifically its high surface tension and oxidation resistance. Fluorine particles undergo a series of polymerization reactions and deposit onto the substrate surface, forming a polymer film with a biomimetic structure. The micro- and nano-scale structures on the coating's surface support liquid molecules, preventing direct contact between the liquid and the substrate, thereby providing effective protection.
(1) Ultra-thin: The coating is nanometer-scale in thickness, ensuring no impact on the dimensions or performance of the circuit board;
(2) Transparent: The coating is colorless and transparent, preserving the circuit board's original appearance;
(3) Eco-friendly: The coating material is non-toxic and pollution-free, complying with international environmental standards;
(4) High-performance protection: Offers excellent water resistance, moisture resistance, oxidation resistance, and corrosion resistance;
(5) Durable and stable: Long-term testing has demonstrated the coating's high durability and stability.
Application of Nano-Protective Coatings on Refrigerator Circuit Boards
A professional team has developed a comprehensive application solution for nano-protective coatings tailored to the specific characteristics of refrigerator circuit boards. During production, the circuit board surface is cleaned, and the nano-protective coating is applied evenly using methods such as spraying, dip coating, or vacuum coating. The coating forms an ultra-thin, transparent protective film that blocks moisture ingress and provides oxidation and corrosion resistance, effectively extending the service life of the refrigerator circuit board.
Refrigerator circuit boards utilizing nano-protective coating technology offer the following advantages:
(1) Enhanced product reliability: Water and moisture resistance reduce the risk of circuit board damage, ensuring the refrigerator operates normally;
(2) Extended service life: Oxidation and corrosion resistance mitigate component aging;
(3) Reduced maintenance burden: Effectively lowers after-sales maintenance costs associated with moisture-related issues;
(4) Enhanced brand image: Delivers a superior product experience for consumers and boosts the competitiveness of the company's core products.
Conclusion
Nanoscale protective coating technology offers a durable and highly effective solution for waterproofing and moisture-proofing refrigerator circuit boards. Adopting this advanced technology not only reduces failure rates during operation and extends product lifespan but also boosts user satisfaction, helping home appliance manufacturers gain market share. As a key trend in the future of the home appliance industry, nanoscale protective coating technology is set to play an increasingly important role in this sector.